测试对比表单页-王设计-鹏瑞图模板
TTR-001 · MILLING
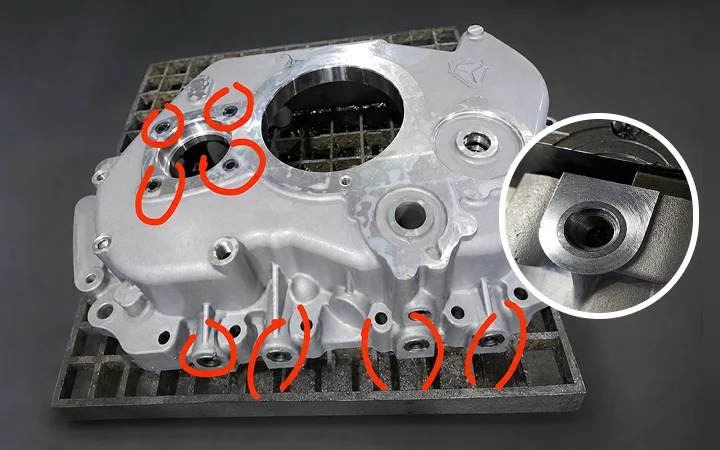
Higher Tool Life and Feed Rate in Gearbox Housing Milling
OBJECTIVE
Compare insert performance in finish and semi-finish milling of a die-cast aluminum gearbox housing with bimetal features.
RECORDED RESULT
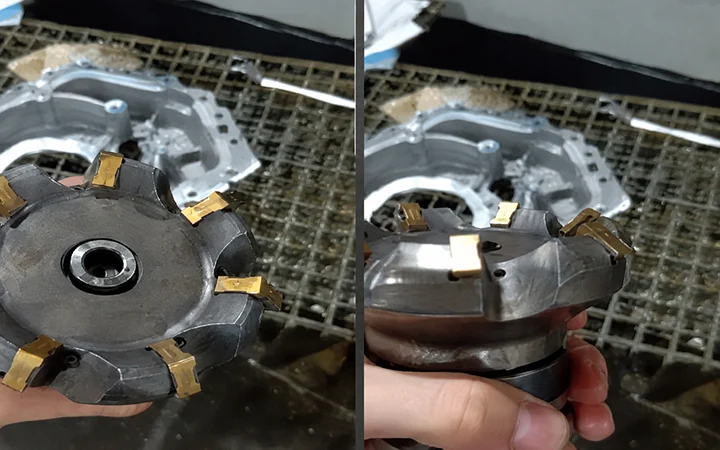
At the same cutting speed and depth of cut, the Premitools insert ran at a higher feed per tooth and recorded 55-60 parts per edge versus 40-45.
0.15 mm/z
Feed Per Tooth
55–60
Parts Per Edge
| TEST ITEM | COMPETITOR | PREMITOOLS TEST TOOL |
|---|---|---|
| Workpiece | Bimetal gearbox housing | Bimetal gearbox housing |
| Material | Die-cast aluminum | Die-cast aluminum |
| Operation | Finish/semi-finish milling | Finish/semi-finish milling |
| Insert | SNMX1206QNN | SNMX120508-M |
| Grade | Competitor | TP8215P |
| Brand origin | South Korea | China |
| Holder | Not recorded | FM88-080A27SN12-Z06 |
| Cutting speed, Vc | 251 m/min | 251 m/min |
| Feed per tooth, fz | 0.08 mm/z | 0.15 mm/z |
| Depth of cut, ap | 3-4 mm | 3-4 mm |
| Recorded tool life | 40-45 parts/edge | 55-60 parts/edge |
| Recorded outcome | Edge chipping at change point | Higher recorded output and feed rate |
TEST SCOPE: Specific recorded application result under the listed test conditions; operator feedback is qualitative.
SOURCE NOTE: Successful Cutting Trial Report, page 1. Recorded test conditions only.
TTR-002 · TURNING
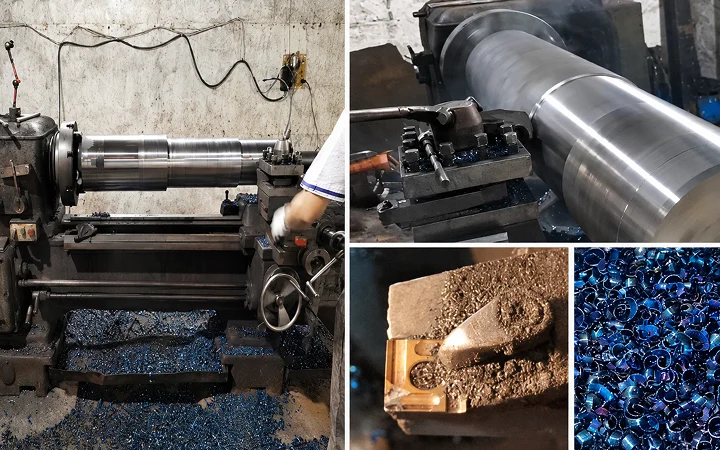
Stable Performance in 38CrMoAlA Injection Screw Turning
OBJECTIVE
Evaluate a Premitools grade against the incumbent insert in semi-finish and rough turning of an injection screw.
RECORDED RESULT
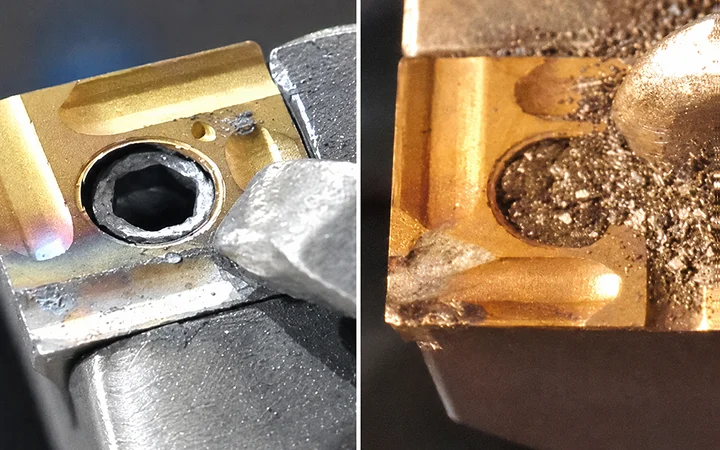
Both tools completed 14 recorded groove sequences. Operator feedback indicated slightly better performance from the Premitools option, although the difference was not large.
14
Recorded Groove Sequences
Matched
Recorded Output
| TEST ITEM | COMPETITOR | PREMITOOLS TEST TOOL |
|---|---|---|
| Workpiece | Injection screw | Injection screw |
| Material | 38CrMoAlA | 38CrMoAlA |
| Hardness | HRC 30 | HRC 30 |
| Operation | Semi-finish / rough turning | Semi-finish / rough turning |
| Insert | SNMG120404R-S | SNMG120404R-S |
| Grade | Competitor | TP9325 |
| Brand origin | Japan | China |
| Holder | PSBNR2525M12 | PSBNR2525M12 |
| Cutting speed, Vc | 140 m/min | 140 m/min |
| Feed | 0.4 mm/rev (as recorded) | 0.4 mm/rev (as recorded) |
| Depth of cut, ap | 6.5 mm | 6.5 mm |
| Recorded tool life | 14 groove sequences | 14 groove sequences |
| Recorded outcome | Incumbent benchmark | Matched output; slightly better operator feedback |
TEST SCOPE: Specific recorded application result under the listed test conditions; operator feedback is qualitative.
TTR-004 · MILLING
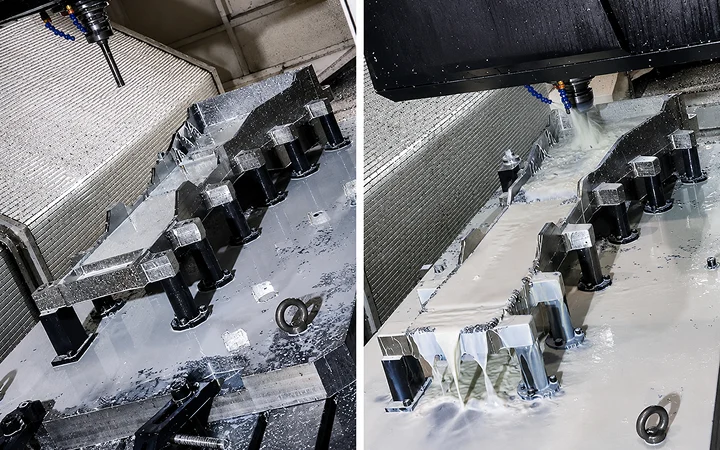
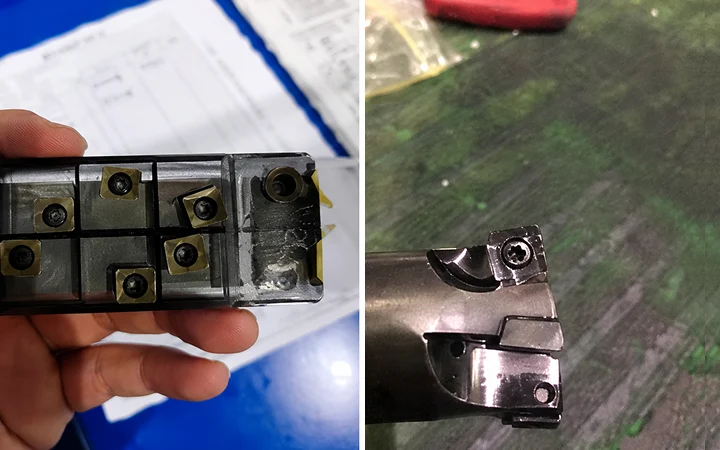
Two More Hours of Tool Life in TC4 Aircraft Beam Milling
OBJECTIVE
Compare insert life in rough milling of a TC4 titanium-alloy aircraft beam section.
RECORDED RESULT
Under the same listed cutting speed, feed and depth of cut, the Premitools option recorded eight machining hours versus six hours for the incumbent.
8H
Recorded Tool Life
+2H
vs. Incumbent
| TEST ITEM | COMPETITOR | PREMITOOLS TEST TOOL |
|---|---|---|
| Workpiece | Aircraft beam section | Aircraft beam section |
| Material | TC4 titanium alloy | TC4 titanium alloy |
| Hardness | HRC 30 | HRC 30 |
| Operation | Rough milling | Rough milling |
| Insert | R210-090414E-MM | SDMT090307-SM |
| Grade | Competitor | TP1815 |
| Brand origin | Sweden | China |
| Holder | R210-035A32-09H | P110-35Z05SD09-M16 |
| Cutting speed, Vc | 71 m/min | 71 m/min |
| Feed | 1 (as recorded) | 1 (as recorded) |
| Depth of cut, ap | 0.6 mm | 0.6 mm |
| Recorded tool life | 6 hours | 8 hours |
| Recorded outcome | Incumbent benchmark | 2 additional recorded machining hours |
TEST SCOPE: Specific recorded application result under the listed test conditions; operator feedback is qualitative.
NEED A TRIAL FOR YOUR APPLICATION?
Share Your Workpiece and Cutting Conditions. Send us your material, operation and current tool setup. Our team will review your application and discuss a suitable insert recommendation or trial plan.